High Speed Laser Cutting for Thin Metal Parts
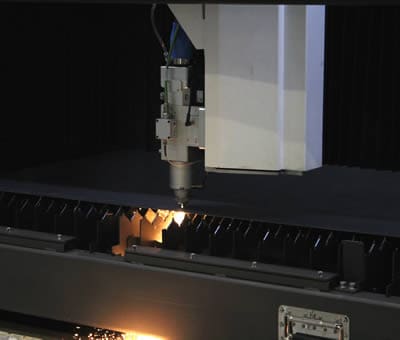
High Speed Laser Cutting Services
Call 0121 544 5808 Today
Bespoke Manufacturing
Instant Quote Service
Worldwide Delivery
Various Gauges/Thicknesses
Bespoke Manufacturing
Instant Quote Service
Worldwide Delivery
Various Gauges/Thicknesses
Faster feed rates put less heat into each millimetre of cut and shrink the heat-affected zone on thin parts. Past the window, edges roughen.
- A laser’s rated speed is a ceiling, not a setting: the job sets the speed.
- Below: how we provide the service, what speed changes, when a press or knife cutter is better, and what to send.
- Full range: laser cutting services.
How Stephens Gaskets Provides High Speed Laser Cutting
We make laser-cut parts to order at our factory, 19 Hainge Road, Tividale, Oldbury B69 2NR. You send the drawing with the material and grade, the thickness and the quantity. We cut to that specification on the laser cutter we use for thin material and laser-cut shims.
A laser needs no cutting die, so a drawing change between batches does not mean new tooling. The minimum order is £250.
What High Speed Means on a Laser Cutter
Laser cutting speed is quoted three ways, and only one of them is the speed of the cut.
| Speed | What It Measures | Where You See It |
|---|---|---|
| Positioning speed | Head travel between cuts, beam off | Machine spec sheets |
| Cutting speed (feed rate) | Head travel along the cut, beam on | Cutting charts for each material and thickness |
| Cycle time per part | Pierce, cut, move and unload for the whole part | Your quote and your lead time |
Ask any supplier for the cutting speed on your material and thickness, not the positioning speed.
Speed Sets Heat Input
Line energy is laser power divided by cutting speed, in joules per millimetre of cut. At a fixed power, doubling the speed halves it.
| Laser Power | Cutting Speed | Line Energy |
|---|---|---|
| 1,000 W | 10 m/min | 6.0 J/mm |
| 1,000 W | 20 m/min | 3.0 J/mm |
Less heat per millimetre generally gives a smaller heat-affected zone, the band along the cut where the metal has taken enough heat to change. In one study of 1.5 mm mild steel cut with a fibre laser and oxygen, the lower speed gave a larger heat-affected zone and a wider kerf on the beam-entry side.
On a small, thin part there is little metal between one edge and the next, so that band is a larger share of the part.
Why Faster Is Not Always Better
Speed has a ceiling set by edge quality. In a study of 304 stainless cut with nitrogen, dross was worst at the lowest speed and edge roughness was highest at the highest speed [3]. In the mild steel study, the kerf on the exit side was wider at the higher speed, which the authors put down to heat building up. The usable window sits between the extremes.
Both studies are small, so read them for direction. None of their speeds are quoted here because they do not carry over to another laser, gas or thickness.
For a shim the consequence is direct. A shim exists to set a gap to a stated thickness. Dross or a burr standing proud of the face changes that thickness locally, so a fast cut that leaves one moves the cost into deburring and inspection.
Fibre or CO2: What Changes on Thin Metal
Fibre laser cutting and CO2 laser cutting differ first in wavelength: fibre sources typically operate at 1,060 nm and CO2 sources at about 10,600 nm. One machine supplier, Selmach, says the shorter wavelength lets the material absorb more of the beam’s energy instead of reflecting it, and that on thin gauge fibre is “twice or even three times as fast” as a comparable CO2 laser [4]. That is a supplier’s claim. The gain depends on the metal, the thickness and the machine it is compared with.
For laser cutting thin metal, the source is one input to the speed window, so ask any supplier, including us, which one it runs and what thickness range it cuts before you send a drawing.
Real Throughput Is Set by More Than Feed Rate
Cutting speed is one term in the time a part takes. The others do not change when the feed rate does.
| Factor | What It Changes | Does a Higher Feed Rate Help? |
|---|---|---|
| Pierce time | Time per internal hole or slot, so parts with many features | No |
| Positioning between cuts | Time moving between features | Only through positioning speed |
| Nesting | Parts per sheet, so material cost per part | No |
| Handling and sorting | Time to unload and separate small parts | No |
| Set-up and file preparation | Fixed time per batch | No |
Laser, Press or Knife Cutter: Choosing the Route
Speed is one input to which machine should cut a part. Tooling cost against quantity usually decides the rest.
| Route | Suited To | Tooling |
|---|---|---|
| Laser cutter | Thin material and laser-cut shims; prototypes and short runs; drawing changes between batches | No cutting die |
| Powerpress | High-volume OEM production, once the tool has paid back | Press tool required |
| Atom CNC knife cutter | EPTFE and other non-metallic gaskets | No tooling or die charges |
Crossover quantity = tooling cost ÷ saving per part, where the saving per part is the laser cost per part less the press cost per part.
With £1,000 of press tooling, a laser cost of £1.00 a part and a press cost of £0.50 a part, the crossover is £1,000 ÷ £0.50 = 2,000 parts.
Check: the laser costs 2,000 × £1.00 = £2,000, and the press costs £1,000 + 2,000 × £0.50 = £2,000.
Below 2,000 parts the laser is cheaper; above it the press is. These are illustrative figures, not our prices.
EPTFE and Non-Metallic Gaskets: A Different Machine
EPTFE and other non-metallic gasket material goes to the Atom CNC knife cutter, which needs no tooling or die charges. TWI advises that laser cutting of fluoropolymers “should be the subject of a rigorous risk assessment” and notes that PTFE can cause polymer fume fever when overheated.
FAQs
What does high speed laser cutting mean?
Is faster laser cutting speed always better?
What is the difference between fibre and CO2 laser cutting on thin metal?
Can brass and copper be laser cut?
Can PTFE and EPTFE gaskets be laser cut?
When is a press tool cheaper than laser cutting?
What is the minimum order?
What to Send With Your Enquiry
A quote needs the same few facts whichever machine cuts the part:
- Material and grade, as written on your drawing or material certificate.
- Thickness, with the tolerance on it.
- Quantity per batch and the quantity you expect over a year.
- Critical dimensions and their tolerances.
- Edge requirements, such as no dross on the sealing face or which side the burr may sit.
- Your drawing, and whether you supply the material.
Below 0.5 mm the standard’s range does not apply, so put the tolerance on the drawing. Tolerances for laser-cut parts are covered on our laser cutting tolerances page.